Infant Formula & Milk Powder Packing
Independent advice on infant formula and milk powder packing: consistent bulk density, reliable scoop dose, correctly sized cans, gas systems, fill accuracy and seal integrity.
Practical support for line specification, supplier selection, operating improvements and staff training. Watson Dairy Consulting is independent of packing-equipment suppliers.
Infant Formula: Bulk Density, Scoop Weight and Nutrient Dose
For infant formula, consistent bulk density is critical to both the pack and the dose. At a fixed declared weight, it affects powder height and the airspace in the can. In a fixed-volume scoop, it affects the grams of powder delivered and therefore the energy and nutrients in the prepared serving.
The scoop, powder characteristics, declared composition and preparation instructions need to be validated together. A correctly weighed can does not, by itself, prove a consistent scoop dose.
From scoop volume to powder mass
Scoop volume (mL) × effective scoop-fill density (g/mL) = grams per scoop
Use the supplied scoop and the intended filling and levelling method. Measure actual scoop weights; do not assume that a laboratory poured or tapped bulk-density result equals the density achieved in a scoop.
From powder mass to energy
Number of scoops × verified grams per scoop × product energy (kcal/g) = kcal per serving
To express this per 100 mL, use the final prepared volume. The water added and the final volume are not necessarily the same because the powder contributes to the volume. [1]
Engineering illustration only, not a feeding instruction: a 10 mL scoop filled at an effective density of 0.45 g/mL delivers 4.5 g. At an illustrative 5 kcal/g, that is 22.5 kcal per scoop. If effective density rises by 10% to 0.495 g/mL, the same scoop holds 4.95 g and 24.75 kcal. At the same scoop count, powder mass and energy rise by 10%; the change per 100 mL also depends on final prepared volume.
What to control: agree the product's density and scoop-weight acceptance criteria, then check representative lots and relevant filling, settling, handling and storage conditions. Investigate changes from drying, agglomeration, conveying or blending rather than compensating by changing the declared product specification or feeding instructions. Scoop technique itself also introduces variation. [1]
Can Design: Airspace, Reinforcing Beads and Pressure Resistance
Select the can around the required net mass and the validated range of as-filled bulk density. Powder at the lower end of that range occupies more volume and leaves less headspace; a denser powder leaves more headspace at the same mass. Consistency makes the fill height and gas-flushing conditions more repeatable.
Approximate free headspace = usable internal can volume − powder mass / as-filled bulk density − displacement by the scoop and other inserts
Use compatible units and the supplier's usable internal dimensions. For example, 1 kg at 0.4 kg/litre occupies 2.5 litres; at 0.5 kg/litre it occupies 2.0 litres. Both contain 1 kg. Allow for the actual filling and settling process, the closure and the scoop.
- Height and diameter: check powder fill height, space to insert and retrieve the scoop, closing clearances and the filling nozzle's reach and position. The external can dimensions do not establish usable volume.
- Gas access: assess the route and time available for flushing. There is air between powder particles as well as in the visible headspace; increasing headspace alone will not remove interparticle air.
- Can strength: agree the wall gauge, reinforcing beads, end design and seam specification with the can supplier. Validate the assembled can against the expected inward and outward pressure differences, handling and transport conditions.
- Trials: combine the actual powder, can, scoop, gas mixture and closing conditions. Check fill height, closure cleanliness, gas composition, pressure and dimensional stability after equilibration and through the intended distribution conditions.
There is no universal headspace percentage or can height suitable for every formula. Do not solve a capacity problem by reducing the required net contents.
Critical design requirement: match the can to the gas and distribution route
The can structure and N₂/CO₂ system must be designed and validated together. Excessive CO₂ uptake can reduce internal pressure until the can pulls inward or buckles if its vacuum resistance is exceeded. Outward pressure can instead bulge the ends or overload the closure. The design must cover filling conditions, gas equilibration, temperature and the pressure changes along the actual transport route.
Why many cans have ridges: circumferential reinforcing beads stiffen the body and help resist radial buckling under an inward pressure load. Their profile, depth and spacing work with the can's diameter, height, metal thickness and material properties. Specify the can's tested performance, rather than judging strength by appearance or bead count. Ends and seams also require suitable resistance. [15] [16]
Inward load: pulling-in or panelling
This occurs when outside pressure exceeds inside pressure. CO₂ absorption and cooling can lower internal gas pressure. Moving to a lower elevation raises outside pressure and, with other conditions unchanged, increases the inward load.
Outward load: bulging or blowing
This occurs when inside pressure exceeds outside pressure. Moving to a higher elevation lowers outside pressure and, with other conditions unchanged, increases the outward load. Warming or CO₂ release from the product can also raise internal pressure.
The combined effect decides the outcome. A can can still pull inward at high elevation if absorption or cooling lowers its internal pressure sufficiently; it can bulge at low elevation if its internal pressure remains higher than ambient. Elevation alone does not establish the failure direction. The relevant load is the difference between the internal and external absolute pressures. [3] [17]
What to put in the specification: the can material, wall thickness, height/diameter, bead design, ends and seams; agreed inward- and outward-pressure limits with an appropriate design margin; and the validated N₂/CO₂ operating range. Record the sealed-can pressure and temperature at filling and after equilibration. Test representative filled cans through the expected temperature and ambient-pressure extremes, including relevant mountain routes or air freight, then check deformation, seams and package integrity. Gas-supply pressure alone does not establish sealed-can pressure. [16]
Nitrogen / CO₂ Mixtures, Fat Absorption and Can Pressure
Nitrogen helps displace oxygen and has low solubility in the product. Some powder systems use nitrogen with carbon dioxide. The mixture must suit the formulation, can and intended distribution conditions; a published or supplier example is not a universal operating recipe. Air in the powder may require pre-gassing as well as headspace flushing.
CO₂ absorption into fat and the powder
CO₂ can dissolve in the fat and be taken up by the powder, reducing the amount remaining in the gas phase. This is different from oxygen being consumed by fat oxidation. Uptake depends on formulation, CO₂ partial pressure, temperature, time and the physical state of the fat; it cannot be predicted from fat percentage alone. Milk-fat research shows that the liquid/solid fat balance matters. [2]
Published infant-formula work models the interaction between CO₂ absorption, temperature and package pressure. Use that principle with product-specific data and the can supplier's pressure limits, as explained in the can-design requirement above. [3]
Validate quality as well as pressure. One infant-formula study found that the higher-CO₂ treatments affected pH and acidity. That supports product-specific trials, not a blanket rejection or recommendation of CO₂. Gas flushing does not sterilise powder or replace hygienic manufacture. [4]
Measure oxygen, CO₂ and the time after filling
Specify the required gas composition, sampling method and measurement times. Check the blend at the mixer outlet and the atmosphere in finished packs, including a defined later check where product absorption changes the result. A low oxygen reading alone does not prove the correct N₂/CO₂ ratio, an intact seal or an adequate shelf life. Set limits and shelf-life claims from evidence for the actual product, complete pack and storage conditions. [16]
Gas Supply, CO₂ Delivery and Mixing-System Design
Decide whether to use a certified premix or blend gases on site. Then size and verify the complete supply route at the line's real demand, including starts, purges, speed changes and simultaneous users. A mixer that gives the right blend at steady flow may need additional control for cyclic demand.
| Design point | What needs to be established |
|---|---|
| Gas supply | Food-grade specification and traceability; nitrogen purity where generated on site; CO₂ source, storage and vaporisation capacity appropriate to peak and sustained demand. [5] |
| Mixer and regulation | Ratio accuracy over the required flow range, inlet-pressure stability, pressure losses and performance during demand changes. Use a buffer receiver where required by the selected mixer design. |
| Distribution | Appropriate piping, isolation, backflow prevention and filtration. Provide controlled delivery to the actual pre-gassing, filling and closing points; check for air ingress and excessive delay before sealing. |
| Measurement and controls | Verify the mixture with appropriate gas analysis. Define low-supply and out-of-ratio alarms, response to faults, and the affected-product hold or reject arrangements. Test restart conditions as well as normal running. |
| Gas use | Record gas consumed per conforming pack, including purge and idle consumption. Compare settings at the same reference conditions and reduce waste only while maintaining validated pack performance. |
| Workplace design | Assess ventilation and gas-monitoring requirements for the installation. CO₂ monitoring has a distinct purpose: an oxygen-deficiency monitor alone does not establish a safe CO₂ concentration. [6] |
Specify blend percentages and volumetric flow on a consistent temperature/pressure reference basis. Do not substitute a mass ratio for a volume ratio. Pressure, receiver size and gas-flow settings must be selected for the particular installation.
Six Practical Packing-Line Checks
Start with the approved product and packaging specification. Record the net-weight limits, gas requirements and sealing settings. Use the site's authorised procedures for adjustments and restart.
1. Fill accuracy and tare
Verify weighing equipment with suitable reference weights and test packs. Check empty-pack variation and actual net contents. Investigate unstable feed, dosing cut-off and differences between filler heads. Weight-based and volumetric filling respond differently to density changes. [7]
2. Product giveaway
Review average net fill, its spread and rejects by head, product and shift. Reduce variation before considering any operating-target adjustment; retain the required product specification, net contents and acceptance limits. [8]
3. Powder in the seal
Check for powder, folds and damage at the closure. Verify approved sealing conditions or can-seam measurements and teardown checks. Relate defects to material lots, machine settings and production conditions.
4. Gas use and composition
Compare gas consumption, O₂ and CO₂ with the approved method and timing. Check supply, blend, flushing points and exposure before closing. Investigate the cause before simply increasing flow.
5. Inspection and rejection
Challenge checkweighing, foreign-body inspection and rejection using the approved procedure. Verify actual removal, reject confirmation and fitted fail-safe controls. A detection signal alone does not confirm rejection.
6. Records and restart
Record results, adjustments, stoppages and losses. Follow the site's stop, hold and escalation procedure when a critical check fails. Complete the required checks after changeover, maintenance and restart.
Seal Integrity and Foreign-Body Inspection
Headspace gas analysis and leak testing answer different questions. Gas analysis checks the atmosphere; closure examination and an appropriate leak test assess package integrity. Low oxygen immediately after flushing does not prove a sound seam. Select and validate the tests for the actual can, pouch or bag. [16]
Specify expected contaminants, detection point and demonstrated sensitivity. Metal-containing packaging can limit conventional metal detection, so the hazard assessment may call for inspection before packing or an appropriate packaged-product system. X-ray has different capabilities and limitations; neither technology detects every foreign body. Verify rejection as part of the complete installation. [9]
Hygienic Filling of Powdered Infant Formula
Powdered infant formula is not sterile. Protect exposed powder after the validated heat-treatment stage through risk-based hygienic zoning, controlled people and material entry, suitable air handling and effective cleaning and drying. The applicable standard and plant hazard assessment determine the controls and zoning terminology. [10]
Approve packaging suppliers and protect cans, lids, scoops and film during storage and transfer. Where UV-C or pulsed light is selected, validate treatment on the actual components at production speed, accounting for positioning and shadowed surfaces. Do not assume that a generic exposure time decontaminates every shape.
Food-Contact Materials: BPA, Can Linings and RTF Packaging Inks
Can linings and bisphenol A (BPA)
BPA has been used in some epoxy can coatings. Specify the complete packaging system, including the can body, ends, coatings, closures and other food-contact components. Obtain the applicable supplier declarations of compliance and supporting assessment or migration evidence for the intended product, contact conditions and shelf life. A “BPA-free” or “BPA not intentionally added” claim alone does not establish the compliance of the whole pack or its alternatives.
EU Regulation 2024/3190, as amended, restricts BPA and certain hazardous bisphenols, with application-specific transitional provisions. Check the destination market and current requirements: Great Britain, Northern Ireland and EU supply cannot simply be treated as one regulatory position. Revalidate coating compatibility and pack performance when changing materials. [11] [12]
Ready-to-feed (RTF) infant formula: migration from printing inks
Printing on the outside does not, by itself, rule out migration. Depending on the pack construction, ink constituents can pass through layers or transfer from a printed surface to the food-contact surface while material is wound or stacked. This second route is called set-off. It can occur before filling, so the final barrier layer alone is not the whole assessment. [13] [14]
- Assess the finished RTF pack: carton or bottle, printed layers, labels, adhesives, coatings, closures and the actual food-contact surface. Review the process used, including aseptic-pack sterilisation or retorting where applicable, and the intended shelf life.
- Ask for evidence: ink-system suitability, drying or curing controls, prevention of set-off, and a migration assessment relevant to the complete pack and liquid formula. A “low-migration ink” description is not sufficient evidence on its own.
- Check relevant substances: include residual solvents, photoinitiators where used, and relevant reaction or breakdown products in the supplier/laboratory assessment. Select testing for the formulation, material structure, contact time and temperature.
- Control changes: re-assess changes to inks, print coverage, curing, adhesives, laminate structure, suppliers and processing conditions. Retain traceability to packaging lots.
This RTF assessment is separate from dry-powder gas flushing. These are packaging specification and verification points, not a claim that current printed packs are generally unsafe. Check the rules and supporting evidence for each intended market.
New Lines, Upgrades and Staff Training
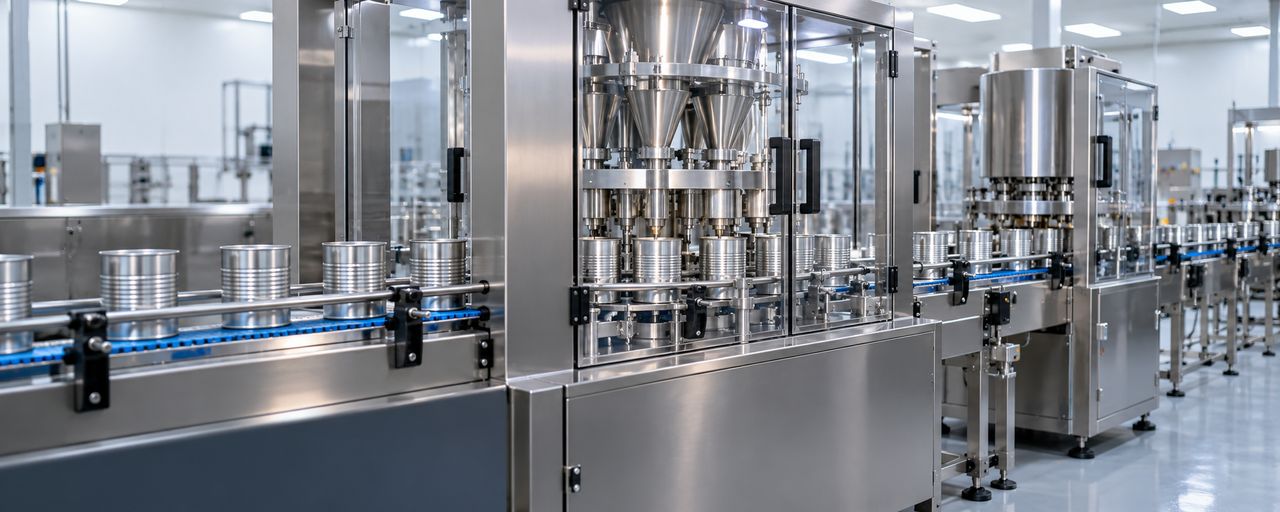
Support can cover big bags, sacks, infant-formula cans, pouches and sachets, with inspection, coding, case packing and palletising. For a new or second-hand line, assess the actual product and pack range, condition, hygienic design, controls, spare parts and refurbishment needs.
- Define conforming output: distinguish running speed from good packs per shift, including the actual changeovers, cleaning, stops and rejects.
- Agree acceptance trials: use representative powders and packaging; measure fill variation, scoop handling, gas composition, seal integrity and sustained output.
- Train for operation: cover setup, authorised adjustment, cleaning, verification, fault response, changeover and restart with the people who operate and maintain the line.
- Measure the benefit: compare baseline and follow-up records for giveaway, powder losses, gas use, rejects, downtime and conforming output. Base savings on the site's data.
Bring the product and pack specification, density and scoop data, fill-weight records, gas results and recurring faults. Watson Dairy Consulting can help identify practical changes and define acceptance checks.
Frequently Asked Questions
Why is bulk density critical for infant formula?
Density affects the volume occupied by a fixed mass and the mass delivered by a fixed-volume scoop. Grams per scoop multiplied by product energy per gram gives energy per scoop. Validate actual scoop weights, composition and preparation instructions together; a correctly weighed can alone does not establish a consistent scoop dose.
How should can size and headspace be selected?
Use the required net mass, validated as-filled density range and usable internal can volume. Allow for filling, settling, the scoop, closing and gas access. Consistent density makes powder height and headspace more repeatable. Validate can strength against the expected pressure differences and distribution conditions.
Why do many powder cans have reinforcing ridges?
Circumferential ridges, or beads, stiffen the can body and help resist radial buckling under an inward pressure load. Their design works with the can dimensions, material and wall thickness. Specify tested pressure resistance for the body, ends and seams; appearance or bead count alone does not establish strength.
How do CO2 and elevation affect can distortion?
CO2 uptake can lower internal pressure. Higher elevation lowers outside pressure and, with other conditions unchanged, favours outward loading; lower elevation favours inward loading. Absorption, temperature and the initial sealed-can pressure can change the outcome. Validate the gas mixture and can together across the intended distribution conditions.
Can CO2 be absorbed into powder fat?
Yes. CO2 can dissolve in fat and be taken up by the powder, changing gas composition and internal pressure. Uptake depends on the product, pressure, temperature, time and fat physical state. Validate the mixture with the actual formulation and package rather than selecting a universal ratio.
What needs checking on a gas-mixing system?
Check food-grade supply, purity, peak flow capacity, pressure stability, mixer operating range, distribution and gas analysis. Verify starts, stops and demand changes as well as steady running. Define alarms and the response to off-specification gas or affected packs.
Does low headspace oxygen prove that a pack is leak-free?
No. Headspace gas analysis measures the atmosphere in a pack. Closure examination and a suitable validated leak test assess package integrity. A low initial oxygen reading alone does not establish a sound seal.
Does higher bulk density cause an underweight pack?
Not automatically. Density changes the volume occupied by a given mass. A volumetric filler can deliver a different mass when density changes; a weight-controlled filler should deliver the specified mass, subject to verified equipment performance. Checkweighing and tare control remain necessary.
Is a BPA-free claim enough to approve a can?
No. Assess the complete pack and obtain the applicable supplier compliance declarations and supporting evidence for the intended product, contact conditions and market. Alternative coatings and components also need assessment. Check the relevant current rules and transitional provisions.
Can outside printing affect ready-to-feed formula packaging?
Depending on the construction, ink constituents may pass through packaging layers or transfer to the food-contact surface while material is wound or stacked. Assess the complete RTF pack, drying or curing controls, set-off prevention and migration evidence for the actual formula, process and shelf life.
What pack formats do you cover?
Big bags, sacks, cans, pouches and sachets for milk powders and infant formula, with inspection and downstream integration matched to the product and required duty.
What is your fee model?
Day rate plus expenses. No commissions from equipment suppliers. The scope, timing and commercial terms are agreed for the assignment.
Related guidance: infant formula and milk powder, big bag specification, spray dryers, filling equipment and dairy equipment.
Technical References
Academic research, official guidance, standards and independent technical references. Operating limits must be established for the actual product and installation.
- Variability and error in measurement of infant formula powder and water (2024). Experimental research on preparation measurements.
- Investigation of solubility of carbon dioxide in anhydrous milk fat by lab-scale manometric method (2017). Experimental fat-solubility research.
- A Model to Tune Modified Atmosphere Conditions of Powdered Infant Formula Packaging (2017). Absorption and package-pressure modelling.
- Effects of modified atmosphere packaging conditions on quality preservation of powdered infant formula (2018). Formulation-specific storage study.
- EIGA publications: Doc 125, Guide to the Supply of Gases for Use in Foods; Doc 126, Minimum Specifications for Food Gas Applications. Find the current editions in the official catalogue.
- EIGA SI 024/24: carbon dioxide physiological hazards. CO₂ monitoring and exposure assessment.
- OIML R 87:2016: Quantity of product in prepackages. Net contents and tare assessment; apply the relevant local requirements.
- OIML R 51-1: Automatic catchweighing instruments. Metrological and technical requirements and tests.
- FDA: draft preventive-controls guidance, Chapter 4. Discussion of physical-hazard controls, detection capabilities and limitations.
- Codex Alimentarius official portal. Reference: CXC 66-2008, Code of Hygienic Practice for Powdered Formulae for Infants and Young Children.
- EU Regulation 2024/3190, consolidated 23 February 2026. BPA and specified hazardous bisphenols in food-contact materials.
- Food Standards Agency: BPA in food-contact materials, EU rules and UK implications (June 2026). Market-specific application.
- Regulation 2023/2006 on good manufacturing practice, consolidated March 2025. Printing-ink transfer and set-off controls.
- Fraunhofer IVV: migration of UV printing inks. Research into migration and set-off.
- Public patent US9382034B2: Strengthened food container and method. Original technical disclosure of circumferential beads and radial loads; no patent-specific pressure rating is adopted here.
- Campden BRI: food-packaging metals testing. Can-body strength, pressure, vacuum and seam assessment.
- NOAA: air pressure. Atmospheric pressure decreases with increasing elevation; gas pressure also changes with temperature.
John Watson
Office: +44 1224 861 507
Mobile: +44 7931 776 499
jw@dairyconsultant.co.uk
We are a longstanding member of the Society of Dairy Technology
and have Fellowship of the Institute of Food Science and Technology.

Contact Details
John Watson
Office: +44 1224 861 507
Mobile: +44 7931 776 499
jw@dairyconsultant.co.uk
What Our Clients Say
We are a longstanding member of the Society of Dairy Technology
and have Fellowship of the Institute of Food Science and Technology.
Locations
Services
Enquiry Form

